 简体中文
 Japanese
 Korean
 Russian
 繁体中文
 Español
Valve selection
Do we still need to verify the on-site system pressure test if the valve passes the factory test?
The objects of factory testing and on-site system pressure testing are different. The customer provides the segmented boundary, valve position, and pressure on both sides to the project party for confirmation, and checks the shell, valve seat, and lining conditions separately, without expanding the scope of application of one report.
The objects of the factory finished products are different from those of the on-site systems
The factory documents specify the corresponding inspection items and conditions, and the assembled system has new connections and construction status. Flanges, pipelines, instruments, and adjacent equipment together form the site boundary, and installation inspections cannot be ignored just because the valves are qualified. The on-site test plan should be determined by the corresponding design and management procedures.
Technical confirmation should specify applicable standards, media, temperature, and acceptance range, and not recommend a uniform test rate or holding time for all valves. When there are different limitations in the actual system, the project evaluation cannot temporarily replace the entire design with the description of the lowest priced product.
The pressure bearing of the valve body and the pressure difference on both sides of the closure are not the same thing
During the system pressure test, if a valve is closed, it may bear the differential pressure on both sides; This is different from the state where both sides are compressed together. The nominal rating and shell test records of the valve cannot automatically prove that the valve seat meets the requirements at this differential pressure. The test boundary should clearly define the valve position and pressure conditions of each section.
The check structure, enclosed chamber, and segmented connection may affect the charging and discharging paths. Without a complete plan, it is not possible to infer that there is no residual pressure at all positions solely based on the pressure gauge returning to zero. The article does not provide a sequence of on-site pressurized operations, which will be carried out by personnel with responsibilities according to the approved plan.
Lining and non-metallic components have their own limitations
The corresponding temperature, medium, and structural conditions are required for the liquid receiving lining, valve seat, or other non-metallic components. The short-term test meets the requirements of the shell, but it does not mean that negative pressure, cleaning, or other processes can be ignored. The experimental medium and subsequent cleaning delivery should also be organized according to project requirements.
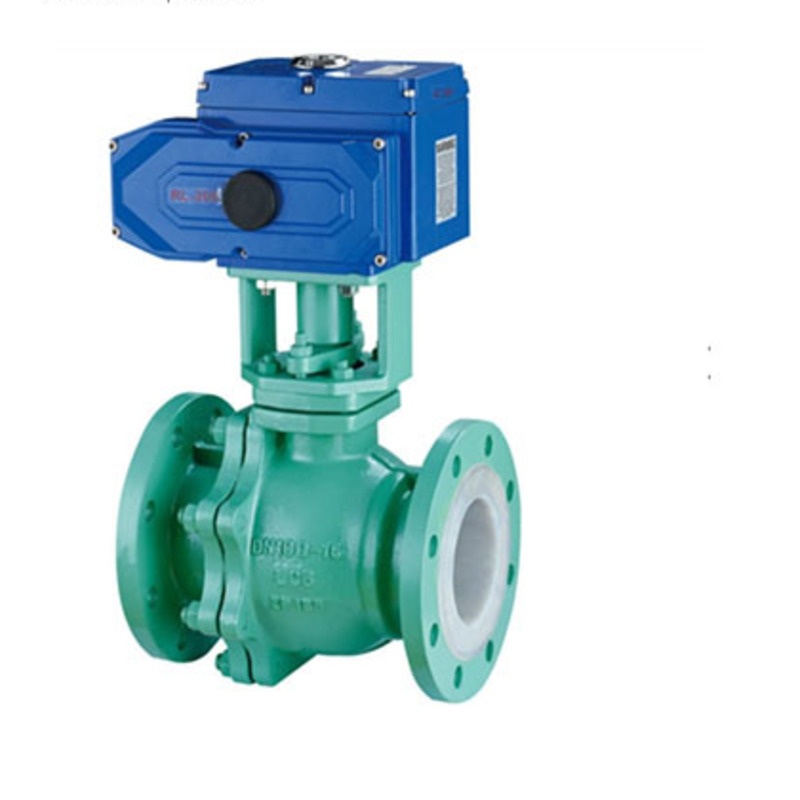
The actual allowable conditions for the electric fluoropolymer-lined ball valve on this site are confirmed by the materials, structure, and documents of this project. The information provided by the external lining manufacturer is only used to illustrate the general boundary and does not apply its magnification or torque meter to the finished products on this site. When using different configurations, corresponding evidence is required.
The actuator is not an infinite pressure differential tool for on-site testing
If action is required during the experiment, confirm the actual load and control conditions. Just because it can be turned on and off during operation, it cannot be assumed that it can also operate under any test differential pressure. The actuator, valve shaft, and sealing force must be consistent with the plan, and should not be forcibly operated without verification.
Handle exceptions according to approved procedures, and prohibit using increased torque, bypass protection, or repeated jogging to remedy unknown blockages. Check the actual valve position, feedback, and complete set status after the experiment. As long as the system pressure does not decrease, it does not mean that the actuator and all functions have been qualified.
Acceptance records should distinguish between manufacturing and installation evidence
Save the factory report, on-site plan, and actual measurement records, respectively indicating which part has undergone what inspection. After installation changes or repairs, the original file coverage needs to be rechecked. The report number should correspond to the product identity and avoid using similar samples as evidence for this document.
After the on-site test is completed, the recovery shall be confirmed according to the project procedure, and the requirements for cleaning, drying, and protection shall not be omitted. If the test results are abnormal, locate the specific path and conditions before handling, do not deny the on-site problem as "the manufacturer has already tried", and do not attribute all construction problems to the finished product.
Valve confirmation items before system testing
| Verify project | Clear information is required |
|---|---|
| scope | Test segmentation, connection, and adjacent equipment |
| condition | Medium, temperature, pressure, and pressure difference of each section |
| structure | Valve seat, lining, valve chamber and allowable valve position |
| complete set | Action load, protection, and post test functionality |
Corresponding products and further reading
The factory report and on-site test each provide different evidence. Distinguishing between finished products, installation, and system boundaries, and then checking the pressure difference against the complete set of conditions, is necessary to avoid expanding a one-time qualification into unlimited applicability.
Can be combinedElectric fluoropolymer-lined ball valveData compilation for this working condition; See for similar structuresElectric ValveColumn. The specific configuration and delivery basis need to be confirmed separately.
Extended reading:What is the difference between pinhole inspection and pressure testing for fluoropolymer-lined valves? Acceptance evidence cannot replace each other。
General technical basis:Example of installation and pressure test boundary for CRP lining systemThe specific configuration and rated conditions of the finished product shall be subject to the information provided in this supply.
Which section of boundary does the valve bear in the on-site plan
List the test sections, valve positions, pressure status on both sides, and adjacent equipment on the same diagram, and have the project personnel confirm whether they meet the finished product limitations. We cannot just give a full line test pressure and let the installation personnel guess what differential pressure the valve seat is subjected to when closing. Factory reports and on-site records shall be kept separately.
Common customer questions
Are all on-site pressure testing conditions applicable if the factory test is qualified?
No. The on-site objects and conditions are different, and it is necessary to verify the system scheme, valve seat differential pressure, and finished product limitations.
Can the shell withstand pressure, so it must be able to close the valve for segmented isolation?
It cannot be directly inferred. The differential pressure, sealing performance, and isolation boundary of the valve seat should be confirmed in the actual plan.
Can the electrical torque be increased if it cannot be turned on during on-site pressure testing?
It should not be processed without confirmation. First, check the load, valve position, and cause of abnormalities according to the approved procedure, and do not bypass the protection and forcefully operate.
 Home
 Valve selection
 news information
 Contact us